Drilling and countersinking holes in Hardox or other wear-resistant plate materials is a much more demanding operation than machining standard structural steel. In most workshop environments, these types of holes would normally be produced on large stationary milling, boring, or CNC machines using rigid setups and premium carbide tooling.
However, in many real-world applications, particularly site work, quarrying, mining, heavy plant maintenance, and mobile fabrication, these holes often need to be produced in the field where large machinery simply is not available.
In these situations, a magnetic drilling machine combined with specially designed tungsten carbide tooling provides the most practical and effective portable solution.
It is important to understand that portable machining in Hardox is not intended for high-production work. This is a practical field solution rather than a mass-production process. Operators should not expect tooling life comparable to machining mild steel, and it would be unrealistic to expect hundreds of holes from a single cutter when working in Hardox or similar wear plate materials.
Machining Hardox is considerably more challenging than using a magnetic drill on standard structural steel. It requires more machine stability, higher torque, correct speeds and feeds, proper lubrication, and good operator technique.
When the correct equipment, tooling, and procedures are followed, excellent results can still be achieved safely and effectively in portable applications.
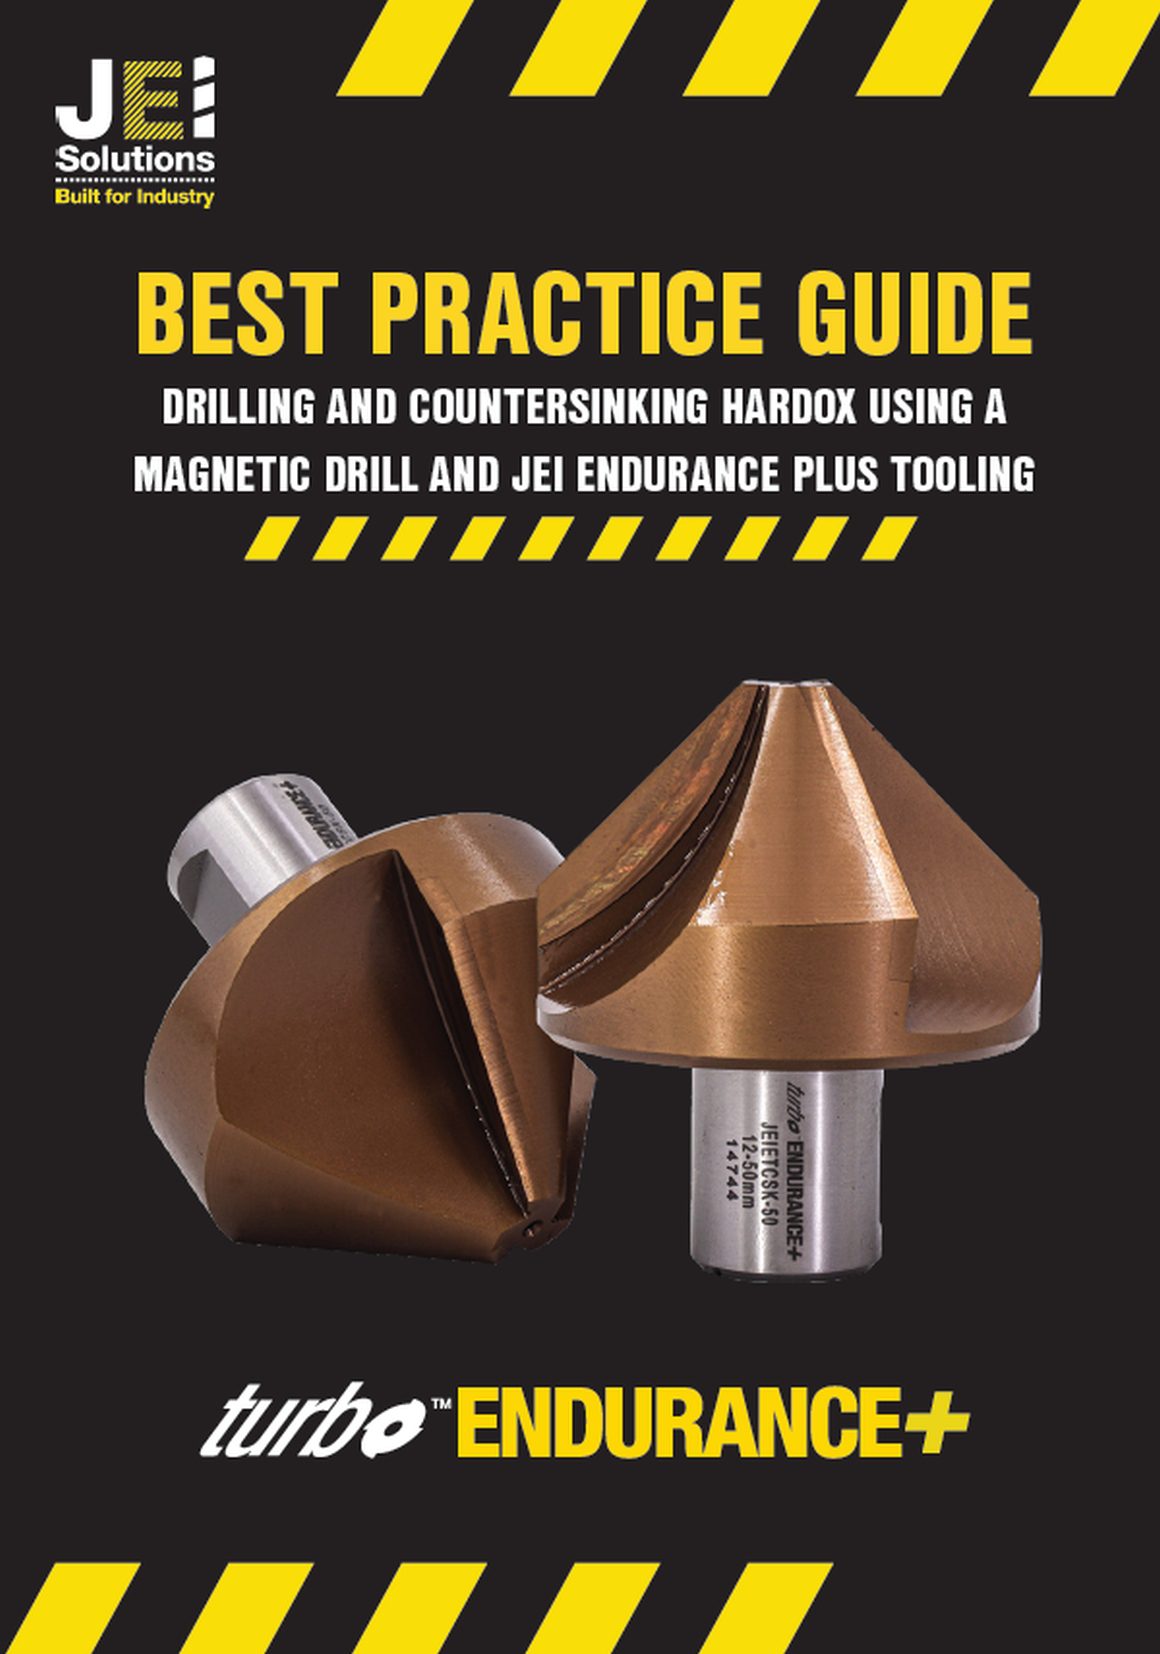
This guide, from the experts at JEI Solutions, outlines the recommended best practice for producing a 22 mm countersunk hole in Hardox 450–500 using a magnetic drill and JEI Endurance Plus tooling.
Although a 22 mm hole is used as the example throughout this document, the same principles apply to larger diameter holes. For larger applications, simply use a larger capacity machine and ensure the correct cutting speeds and feed rates are maintained for the cutter diameter being used.
Portable machining in Hardox is never as straightforward as drilling standard steel, but with the correct machine, tooling, speeds, and lubrication, excellent results can be achieved in the field.
For best results: Use a rigid, high-torque magnetic drill; Maintain lower spindle speeds; Use premium carbide tooling; Apply constant lubrication, keep feed pressure controlled and consistent.
Following these guidelines will help maximise cutter life, improve finish quality, and ensure safer, more reliable operation when machining Hardox wear plate.
www.jeiuk.com